
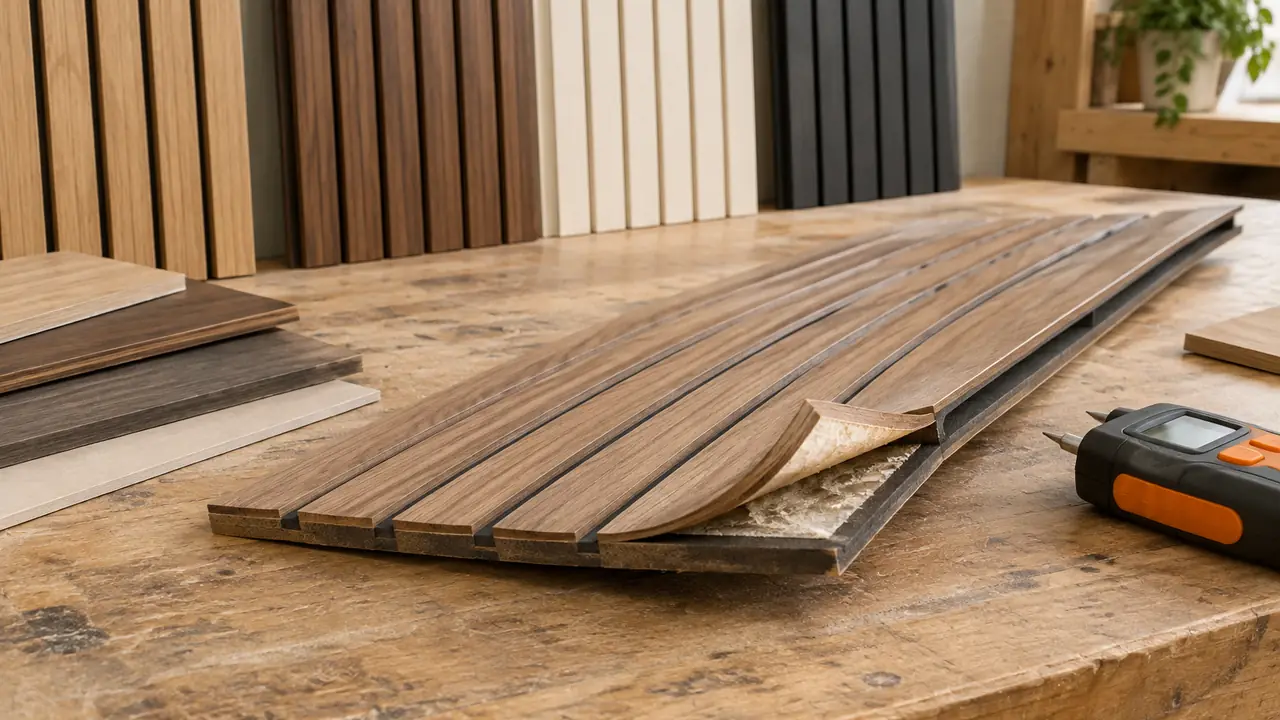
A gap is a sum of tolerances
Every joint on a paneled wall carries the accumulated deviation of everything upstream of it: the wall's flatness, the batten plane, the panel's cut length, the panel's thickness, the reference line the installer worked from, and the building itself, whose floors and ceilings were rarely level to begin with. A "bad gap" is therefore rarely one bad number - it is two good numbers that disagree, repeated down a wall until the eye, which is exquisitely sensitive to parallel lines, files a complaint. This is why gap disputes are so unsatisfying to resolve by photograph and so easy to prevent by agreement.
The eye's sensitivity is the useful fact to design around. Humans forgive an absolutely uniform gap of surprising width and condemn a wandering gap of almost none; a consistent 3 mm joint reads as craft while a gap that breathes between 1 and 5 mm reads as failure. Uniformity, not tightness, is the target - and uniformity is precisely what can be specified, measured and checked, at the plant and on the wall. The causes below are ranked by how often each ends up owning the problem.
First cause: the wall behind
The most frequent origin is the substrate. Masonry runs out of plumb by centimeters over a room's height; drywall undulates between stud lines; old buildings add settled floors and wavy ceilings to the account. A panel is a straight, flat object, and mounting it on a crooked plane produces exactly the wandering reveal customers photograph. The installer's first tool is therefore a straightedge or string line, not a drill: survey the wall, find the high points, and choose the fixing route that can absorb what the survey found - battens packed out where the wall is generous, rails shimmed where it is not. The installation systems guide matches routes to substrates, and the rule the guide repeats is worth repeating here: the thinner the panel, the flatter the plane behind it must be.
This is also the cause with the cleanest division of responsibility, which matters for importers selling through installers: a substrate survey belongs in the install sheet as a required first step, with the acknowledgment line that keeps it on record. Programs that skip it buy the ambiguity of not knowing, on every wall, whose deviation the gap is.
Second and third: the reference line and the batten grid
Second is the working reference. An installer who sets each panel off its neighbor accumulates and magnifies error down the run - panel tolerance on panel tolerance - while an installer who works from a snapped laser line resets the error at every panel and keeps the run honest. It is a one-sentence difference on the install sheet, and it is the difference between a wall that drifts and a wall that does not. Third is the batten grid itself: battens at irregular centers, or packed by eye, hand their irregularity straight through to the panel face. A grid laid to marked centers, checked with the same straightedge as the survey, is what makes the panel's flatness visible rather than theoretical.
Both causes are installation discipline, which is the most common place for gap problems to live and the least expensive to fix: they cost sentences in a document, not changes to a product. The creaking panels note meets the same battens from the acoustic side - a grid that moves also speaks - and the two notes share the same prevention.
Fourth and fifth: panel tolerance and batch mismatch
Fourth is the panels' own tolerance. Panel sizes and thicknesses are manufactured within agreed limits, checked at inspection against the order - that is what a tolerance is for - and on a wall of many panels the limits stack: a run of panels each at one end of the length tolerance produces a cumulative drift that no reference line can hide. The agreement that prevents this is written in the order and verified per lot, and the practical forms it takes are size and thickness sampling in the inspection plan and a cutting plan that leaves the installer adjusting margins rather than accumulating them. The inspection item is standard: the checks the testing and inspection page organizes include size and thickness verification per lot for exactly this reason.
Fifth is the batch cousin of the same problem: pitch that does not continue across panels. On fluted and slat lines, where machined strips commonly run 12-30 mm wide with 15-40 mm gaps across the category, a wall mixing panels from two production runs can carry two slightly different pitches, and the eye catches the interruption instantly even when both runs are within their own tolerances. The prevention is batch discipline - one lot per wall where the program allows, and color-matching-style controls per the batch matching note extended to geometry, not just tone.
The gap types side by side
| Gap | What controls it | Where the agreement lives | Check |
|---|---|---|---|
| Joint between panels | Reference line discipline; panel length tolerance | Install sheet; size sampling in the inspection plan | Straightedge down the run; string line per course |
| Reveal between slats | Tooling pitch; batch consistency | One lot per wall where possible; pitch named in the order | Pitch check across adjacent panels at install |
| Shadow gap at ceiling | Design; the ceiling's own level | Detail drawing before sampling | Set against laser level at first panel |
| Perimeter gap at floor and walls | Building irregularity; trim program | Trim counts from the drawing; skirting and end caps planned | Walk the perimeter with the trim box before fixing |
What gap risk means for a brand
Gaps are a brand-level risk because they arrive through photographs of other people's work: the listing's panels are fine, but the wall a customer built from them wandered, and the review blames the product. The program levers are documentation and design. Documentation: the install sheet's reference-line rule, gap figures and survey step, packed with every order and repeated on the listing content. Design: deliberate details - a shadow gap at the ceiling, a reveal that reads as intention, trims from the matching trim line at perimeters - that give the wall a place to absorb the building's irregularity on purpose rather than by accident. The sheets versus modular note adds the format angle: modular walls joint more often, so they forgive drift better than single-sheet runs.
Specification and inspection: the joint ledger
The closing lines. Specification: nominal sizes and the tolerance limits named in the order, pitch named for profile lines, one-lot-per-wall stated as the plan where quantity allows, and an install sheet that orders the work - survey, grid, reference line, then panels. Inspection: size and thickness sampled per lot against the agreed limits, pitch checked across panels from the same run, records filed with the lot. On the wall, the same document set reappears as the installer's checklist, and the gap a customer sees is the gap the program designed - uniform, deliberate, and nobody's fault.
Reference quantities and production windows sit on the MOQ and lead time page, and the quote form captures formats, pitch and quantities per wall in the same message as color - which is where joint planning belongs.